

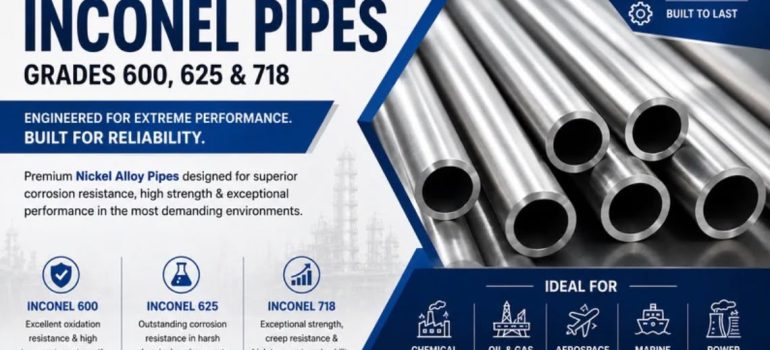
Top Applications of Inconel Pipes in Chemical Processing
Introduction
Chemical processing industries operate in some of the harshest environments where piping systems are continuously exposed to corrosive chemicals, extreme temperatures, high pressures, and aggressive process media. Selecting the right piping material is essential to ensure operational safety, equipment longevity, and reduced maintenance costs.
Inconel Pipes Grades 600, 625, and 718 have become the preferred choice for chemical processing plants due to their exceptional corrosion resistance, superior mechanical strength, excellent oxidation resistance, and ability to withstand elevated temperatures. These nickel-based alloy pipes are engineered to perform reliably in environments where conventional stainless steel and carbon steel pipes may fail.
Mcneil Instrument is a trusted manufacturer and supplier of premium-quality Inconel Pipes Grades 600, 625 & 718, delivering precision-engineered piping solutions that meet international quality standards for demanding industrial applications worldwide.
Why Inconel Pipes Are Ideal for Chemical Processing
Chemical plants handle highly corrosive acids, alkalis, chlorides, solvents, and oxidizing agents that require piping systems capable of maintaining structural integrity under continuous exposure.
Key Benefits
✔ Exceptional corrosion resistance
✔ Superior oxidation resistance
✔ Excellent resistance to chloride stress corrosion cracking
✔ High mechanical and tensile strength
✔ Outstanding heat resistance
✔ Excellent fabrication and weldability
✔ Long operational life
✔ Reduced maintenance costs
✔ Reliable performance under high-pressure conditions
Top Applications of Inconel Pipes in Chemical Processing
1. Acid Manufacturing Plants
Acid production facilities require piping materials capable of handling highly aggressive chemicals such as sulfuric acid, nitric acid, phosphoric acid, and hydrochloric acid.
Inconel Pipes Grade 600 provide outstanding oxidation resistance and excellent durability in high-temperature acid processing environments.
Benefits
- Excellent corrosion resistance
- Long service life
- Reduced downtime
- Improved plant reliability
2. Heat Exchangers
Heat exchangers are continuously exposed to elevated temperatures and corrosive fluids.
Inconel Pipes Grade 625 are widely used because they offer superior resistance to pitting, crevice corrosion, and thermal fatigue while maintaining excellent mechanical properties.
Advantages
- Superior heat transfer performance
- High fatigue resistance
- Excellent weldability
- Reduced maintenance requirements
3. Chemical Reactors
Chemical reactors often operate under extremely high temperatures and pressures while processing aggressive chemicals.
Inconel Pipes Grade 718 deliver exceptional tensile strength, creep resistance, and structural stability, making them ideal for demanding reactor systems.
Benefits
- High structural integrity
- Excellent pressure resistance
- Long equipment life
- Reliable process safety
4. Fertilizer Manufacturing Plants
Fertilizer production involves exposure to ammonia, nitric acid, and corrosive chemical compounds.
Inconel Pipes Grades 600, 625 & 718 provide excellent corrosion protection, helping manufacturers reduce unexpected shutdowns and maintenance costs.
5. Petrochemical Processing Units
Petrochemical facilities require piping systems capable of handling hydrocarbons, corrosive gases, and elevated operating temperatures.
Inconel alloy pipes ensure reliable performance throughout refining and petrochemical processing operations.
Common Applications
- Process piping
- Transfer lines
- Distillation units
- Pressure vessels
- Furnace piping
6. Chlor-Alkali Plants
Chlorine production environments are highly corrosive due to chloride exposure.
Inconel Pipes Grade 625 offer exceptional resistance against chloride-induced corrosion, making them one of the preferred materials for chlor-alkali processing plants.
7. Pharmaceutical Manufacturing
Modern pharmaceutical facilities demand contamination-free piping systems with excellent corrosion resistance and long service life.
Inconel alloy pipes help maintain product purity while providing reliable performance under stringent manufacturing conditions.
8. High-Temperature Chemical Furnaces
Industrial furnaces require piping capable of operating under continuous high-temperature conditions.
Inconel Pipes Grade 600 offer excellent oxidation resistance and maintain mechanical strength even at elevated temperatures.
9. Pressure Piping Systems
Chemical plants operate numerous high-pressure pipelines transporting aggressive chemicals.
Inconel Pipes Grade 718 provide exceptional pressure handling capability and outstanding fatigue resistance for critical applications.
10. Desalination & Water Treatment Plants
Chemical dosing systems and desalination facilities require piping materials that resist seawater corrosion and chemical attack.
Inconel Pipes Grade 625 perform exceptionally well in these aggressive operating environments.
Comparison of Inconel Pipes Grades 600, 625 & 718
| Grade | Key Advantage | Best Chemical Processing Application |
| Inconel 600 | Excellent oxidation resistance | Acid plants, furnaces, heat treatment equipment |
| Inconel 625 | Outstanding corrosion resistance | Heat exchangers, marine chemicals, chlor-alkali plants |
| Inconel 718 | Superior mechanical strength | High-pressure reactors, process systems, gas turbines |
Why Choose Mcneil Instrument?
Mcneil Instrument manufactures premium-quality Inconel Pipes Grades 600, 625 & 718 that comply with international standards and are trusted by industries worldwide.
Our Advantages
✔ Premium nickel alloy raw materials
✔ ASTM & ASME compliant products
✔ Seamless and welded pipe options
✔ Custom sizes and wall thicknesses
✔ Precision manufacturing
✔ Strict quality inspections
✔ Competitive pricing
✔ Worldwide exports
✔ On-time delivery
Industries That Benefit from Inconel Pipes
Our Inconel alloy pipes are extensively used in:
- Chemical Processing Plants
- Petrochemical Industries
- Oil & Gas
- Pharmaceutical Manufacturing
- Fertilizer Plants
- Marine Engineering
- Aerospace Industry
- Nuclear Power Plants
- Heat Exchanger Manufacturing
- LNG Facilities
- Refineries
- Power Generation
Available Types of Inconel Pipes
Mcneil Instrument supplies:
- Seamless Inconel Pipes
- Welded Inconel Pipes
- ERW Inconel Pipes
- EFW Inconel Pipes
- Round Pipes
- Square Pipes
- Rectangular Pipes
- Heavy Wall Pipes
- Thin Wall Pipes
- Custom Fabricated Pipes
Why Industries Prefer Inconel Pipes
Compared with conventional alloy and stainless steel piping systems, Inconel Pipes Grades 600, 625 & 718 provide:
- Longer service life
- Excellent corrosion resistance
- Superior heat resistance
- Reduced maintenance costs
- Improved plant efficiency
- Lower lifecycle cost
- Enhanced equipment reliability
- Outstanding mechanical performance
Conclusion
Chemical processing industries require piping systems capable of delivering long-term reliability under some of the world’s most demanding operating conditions. Inconel Pipes Grades 600, 625 & 718 provide exceptional corrosion resistance, high-temperature strength, and mechanical durability, making them the preferred solution for chemical plants, refineries, pharmaceutical facilities, and petrochemical industries.
Whether you require Inconel Pipes Grade 600 for oxidation resistance, Inconel Pipes Grade 625 for superior corrosion protection, or Inconel Pipes Grade 718 for high-strength applications, Mcneil Instrument offers premium-quality nickel alloy piping solutions designed to meet international standards and exceed customer expectations.
Frequently Asked Questions (FAQs)
1. Why are Inconel Pipes used in chemical processing?
Inconel Pipes offer excellent resistance to corrosion, oxidation, high temperatures, and aggressive chemicals, making them ideal for demanding chemical processing applications.
2. Which Inconel grade is best for chemical plants?
It depends on the application. Inconel 600 is ideal for oxidation resistance, Inconel 625 excels in corrosive environments, and Inconel 718 is preferred for high-pressure, high-strength applications.
3. What industries commonly use Inconel Pipes Grades 600, 625 & 718?
Chemical processing, petrochemical, oil & gas, pharmaceuticals, marine, aerospace, power generation, fertilizer, and nuclear industries.
4. Does Mcneil Instrument manufacture customized Inconel Pipes?
Yes. We manufacture seamless, welded, ERW, EFW, and custom-fabricated Inconel pipes in various sizes, schedules, and wall thicknesses.
5. Why choose Mcneil Instrument for Inconel Pipes?
Mcneil Instrument offers premium-quality products, international manufacturing standards, competitive pricing, global exports, technical expertise, and reliable delivery.


